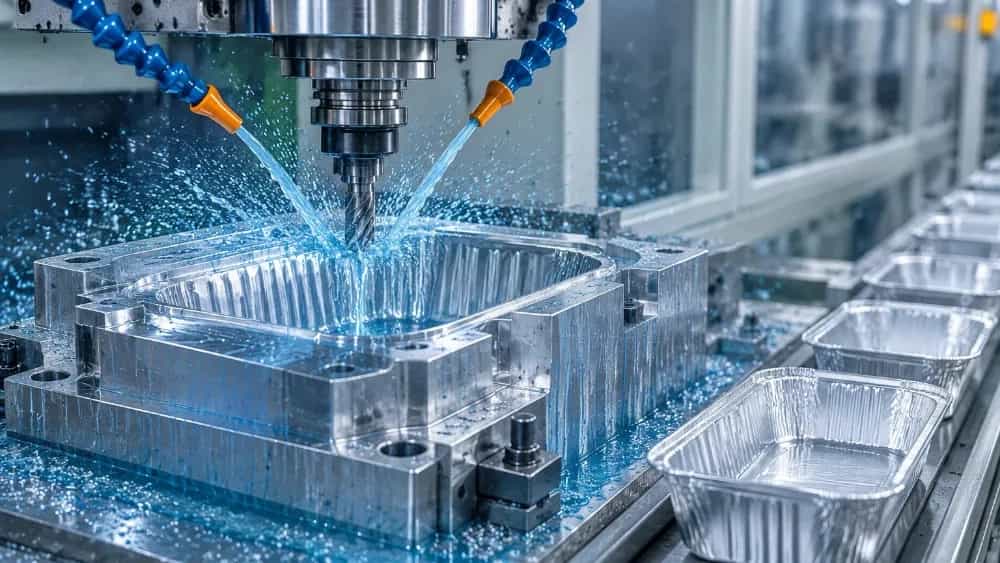
The price of making a mold for disposable aluminum containers depends on the grade of the steel block, the number of cubits or cubits, the precision of CNC machining and the edge cutting system. This cost is calculated based on the type of mandrel and matrix, the air spring mechanism and the thickness of the incoming foil. Before starting the manufacturing process, the customer must specify the exact dimensions of the container and the tonnage capacity of the production line press to estimate the engineering cost.
In automatic food packaging lines, the mold is not just a metal forming tool, but the beating heart of the production line, which determines the return on investment. Operational experience shows that even a fraction of a millimeter of error in the cutting edges of the matrix can cause continuous tearing of the aluminum foil and stop the press line. This issue has made the factors determining the construction cost to be evaluated beyond the raw weight of iron used.
The main variables in calculating the cost of making an aluminum mold
In the technical calculations of molding workshops, the final price is determined based on a set of reverse engineering processes, material type and machining time. Examining the samples implemented in the workshop of Azin Sanat has proven that the separation of costs gives the employer a clearer view to optimize the budget.
Steel grade and heat treatment of mandrel and matrix
Choosing the type of steel has the greatest contribution to tool durability and initial cost. For aluminum container molds, hot work tool steels or alloy steels with high wear resistance such as SPK or standard grades 1.2379 and 1.2344 are usually used. After machining, these steels must undergo vacuum hardening heat treatment so that their surface hardness reaches more than 56 to 60 Rockwell C. The use of poor quality material or traditional heat treatment in an open furnace leads to a dimensional change of the mold and premature wear of the cutting blades.
The number of letters and the nominal circulation of the press
Single-house, two-house or multi-house molds are designed for various circulations. With the increase of the number of covites, the area of the mother block, the volume of simultaneous machining and the complexity of the air exit channels increase in a non-linear way. In the construction of two-door molds, the balance of mandrel pressure in all holes is a condition for the health of the final container, because aluminum foil with a thickness of 45 to 65 microns does not tolerate any unbalanced pressure tolerance.
Cutting system and pneumatic kite mechanism
The big difference between aluminum mold and plastic forming molds is in the peripheral cutting system. The mandrel and die must complete the contouring and cutting of the container in one press stroke. The design of the carbide cutting rings and the pneumatic blowing mechanism to throw the container towards the conveyor belt includes a significant part of the side costs of the standard parts.
Hidden production line challenges that justify the cost of manufacturing
Some buyers, when comparing pre-invoices, only pay attention to the final price difference, while there are hidden parameters that show themselves in the first months of production.
Adapting to the fluctuation of foil thickness in the domestic market
Aluminum foils supplied in the local market do not always have full thickness uniformity. The slack between the mandrel and the matrix should be calculated by the machinist in such a way that with a few microns of sheet thickness fluctuations, the container does not suffer severe folding or cutting of the body. Achieving this tolerance depends on precise spark and wirecut machining, which brings a different operational cost.
Hardness of maintenance and replaceability of consumable parts
An industry standard mold is assembled in a modular way. If the cutting edge slows down after producing hundreds of thousands of blows, it is not necessary to shave the entire surface of the mold; Rather, cutting parts and inserts must be able to be disassembled, ground and replaced separately. Building a modular structure requires more programming and milling time, but it minimizes the repair and maintenance costs of the buyer's factory.
Budget estimation steps in Azin Sanat formatting
In order to reach the real production number, first the physical sample of the desired container, 3D file or packaging design sample is evaluated. Then the tonnage of the employer's hydraulic or mechanical press, the course of the machine and the sheet feeder system are checked so that the dimensions of the mold shoes are made according to the factory standards. Based on the target daily production capacity, Azin Sanat's engineering team suggests the most suitable type of steel and the optimal number of holes so that the useful life of the mold is in full agreement with the initial capital.